Section 1: Executive Overview of Industrial Red Chili Manufacturing & Global Sourcing Standards
In the contemporary B2B food processing landscape, procuring dried chili products (Capsicum annuum L. and Capsicum frutescens) requires a rigorous alignment between agricultural supply chains and industrial processing parameters. Choosing top trusted red chili factories & factory partners is no longer just about commodity pricing; it demands a deep technical evaluation of ASTA color retention physics, Scoville Heat Unit (SHU) stability, micro-sterilization efficiency, and toxicological compliance (such as Ochratoxin A and Aflatoxin limits set by the European Food Safety Authority and the US FDA).
Red chili manufacturing facilities operate as the critical link between agricultural producers and global flavor compound manufacturers, snack seasoning blenders, and pharmaceutical extraction plants. Modern manufacturing protocols mandate full batch traceability, optical color sorting (such as Buhler Sortex technology), continuous stem-cutting mechanisms, and cryogenic milling capabilities to prevent thermal degradation of volatile oleoresins.
Key Analytical Parameters for B2B Procurement Engineers
When evaluating factory-grade dried chili pepper shipments, food technologist buyers prioritize three core quantitative indicators:
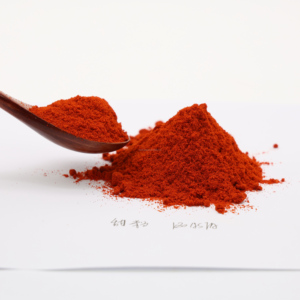
- ASTA Extractable Color (ASTA 20.1): Measured spectrophotometrically at 460 nm. High-grade dried chilis range from ASTA 100 to ASTA 160+. Higher color values indicate dense carotenoid content (capsanthin and capsorubin), which critical for natural food coloring applications.
- Capsaicinoid Content & Scoville Heat Units (SHU via HPLC): High-Performance Liquid Chromatography measures capsaicin, dihydrocapsaicin, and nordihydrocapsaicin. 1 gram of pure capsaicinoid equals approximately 16,000,000 SHU. Varieties vary from low-pungency Paprika (under 2,000 SHU) to high-potency S17 Teja chili (75,000–100,000+ SHU).
- Moisture & Equilibrium Relative Humidity (ERH): Safe storage levels require moisture content below 11.0% (w/w) and water activity (aw) below 0.60 to eliminate Aspergillus flavus growth and mycotoxin synthesis during long oceanic transit.
Information Gain Insight: The Physics of Thermal Degradation in Milling
Traditional hammer milling operates at ambient friction temperatures exceeding 65°C to 85°C. At these elevated thermal states, up to 35% of essential volatile oils are lost to thermal evaporation, and capsaicin structure deteriorates. Advanced red chili factories utilize Liquid Nitrogen (-196°C) Cryogenic Milling. By lowering processing temperatures to under -40°C, volatile oil retention rises to 98.4%, and ASTA color degradation during grinding is virtually eliminated.
Low-Microbial Steam Sterilization
Replacing Ethylene Oxide (EtO) and Gamma Irradiation with High-Temperature Short-Time (HTST) continuous dry steam systems. Reduces Total Plate Count (TPC) to <10,000 CFU/g while fully conforming to organic clean-label legislation.
AI-Powered Sorting & Defect Detection
Deployment of multispectral infrared cameras coupled with AI neural networks to detect micro-aflatoxin mold spores, discolored pods, and foreign plant matter at throughput speeds exceeding 8 tons per hour.
Micro-Encapsulation Technology
Transforming raw capsaicin oleoresins into water-dispersible, thermal-stable encapsulated powders. This permits precise heat-delivery profiles in ready-to-eat meals without causing color degradation during high-pressure thermal processing.
Section 3: Supply Chain Risk Mitigation & EU/FDA Contaminant Control
Global procurement directors face unprecedented regulatory scrutiny regarding agricultural chemical residues and naturally occurring toxins. Key risk vectors in red chili supply chains include:
1. Mycotoxins: Aflatoxin B1, B2, G1, G2 & Ochratoxin A (OTA)
Mycotoxins are toxic secondary metabolites produced by fungi such as Aspergillus flavus during post-harvest sun drying under high atmospheric humidity. Leading chili processing factories combat this risk by transitioning contract farmers from field floor drying to raised solar drying tables equipped with food-grade polycarbonate covers. Furthermore, automated factory lines utilize High-Performance Liquid Chromatography (HPLC-FLD) to guarantee batch levels below EU limits (Aflatoxin B1 < 5 ppb, Total Aflatoxin < 10 ppb, OTA < 20 ppb).
2. Pesticide Residue Control & MRL Compliance
Over 400 active pesticide compounds (including Chlorpyrifos, Profenofos, and Triazophos) are regulated under Maximum Residue Limit (MRL) legislation. Certified factories implement triple-wash pre-treatment combined with LC-MS/MS (Liquid Chromatography-Mass Spectrometry) screening for every incoming lot before crushing or packing.
3. Ethylene Oxide (EtO) Elimination & Allergen Segregation
The global spice industry has witnessed massive recalls due to illegal EtO fumigation used to reduce microbial loads. Top trusted red chili factories employ dedicated HTST vacuum steam sterilization facilities, guaranteeing ZERO EtO residues, while managing strictly allergen-free lines (preventing cross-contact with mustard, sesame, or gluten).
Section 4: Enterprise Processing Infrastructure & Quality Control Assurance
Reflecting the manufacturing leadership inherited from integrated processing operations, top-tier factories utilize a closed-loop quality control workflow from raw pod intake to vacuum-sealed sea-freight packing:
- Step 1: Mechanical De-Stoning & Winnowing: Air separators remove dust, stones, field debris, and metallic particulates.
- Step 2: Optical Stem Cutting & Color Sorting: Automated mechanical blades cut stems precisely at the pod crown, minimizing seed loss while optical sorting discards pale or damaged pods.
- Step 3: Moisture Normalization Drying: Pods pass through indirect hot-air tunnel dryers to ensure uniform moisture content (<10.5%).
- Step 4: Cryogenic Granulation & Milling: Closed-circuit stainless steel mills grind chilis into precise mesh sizes (ranging from 5 mesh coarse crushed flakes to 100 mesh fine powder).
- Step 5: Metal Detection & X-Ray Inspection: Dual-channel metal detectors (Fe, Non-Fe, SS 316) combined with X-Ray inspection guarantee zero physical contamination.
- Step 6: Nitrogen-Flushed Vacuum Packaging: Multi-layer foil bags lined with oxygen absorbers prevent ASTA color degradation and oxidative rancidity during oceanic transit.
In-House Analytical Testing Laboratory
Equipped with HPLC, GC-MS, and spectrophotometers. Every batch is supplied with a certified Certificate of Analysis (COA) covering ASTA color, SHU heat level, moisture, ash content, and microbial counts.
Scalable Annual Output & Storage
Over 550,000 equivalent material meters/tons processed annually. Cold-storage infrastructure capable of holding 15,000 metric tons at controlled 4°C to maintain ASTA stability year-round.
OEM & Tailored Mesh Size Milling
Custom particle sizing (Crushed Flakes with/without seeds, 20-40 mesh pizza topping grade, 80-100 mesh fine industrial powder) tailored to exact client product matrixes.
International Regulatory Compliance
Full compliance with BRCGS (Grade AA), ISO 22000:2018, HACCP, US FDA Registration, Halal, and Kosher certifications for seamless global customs clearance.