Featured Wholesale Food Ingredients & Spices
Explore our core portfolio of sulfur-free botanicals, cryogenic BQF fruits, and premium whole spices certified for global export and industrial food processing.
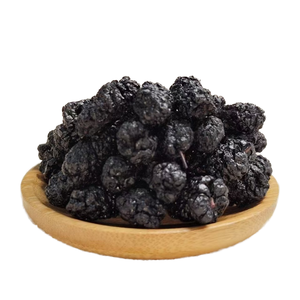
Factory Direct Original Ad Dry Brine Marinated BQF Frozen Black Mulberry 15kg Soft Texture Natural Flavor Raw Herbs Spices
Inquire Now
Small Packaged White Pepper Whole Spices 50g Dried Spicy Food Seasoning for Cooking
Inquire Now
Premium Selected Sulfur Free Dried Star Anise For Cooking Seasoning, Marinating Ingredients And Spices Herbs Products
Inquire Now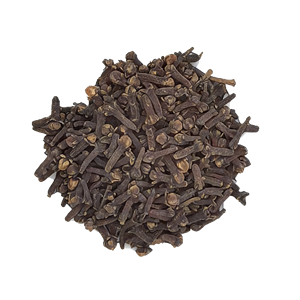
Premium Whole Cloves Natural Intense Aromatic Spice Dried Flower Buds for Cooking Baking Marinating Beverage Blends
Inquire Now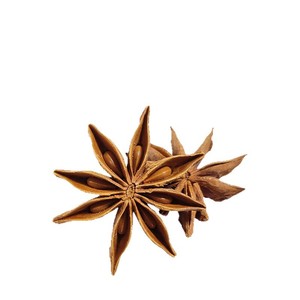
Spring-flower Star-anise Sulfur-free Whole Dried Spices Wholesale Braised-food Seasoning Catering Commercial Use Packaged Food
Inquire Now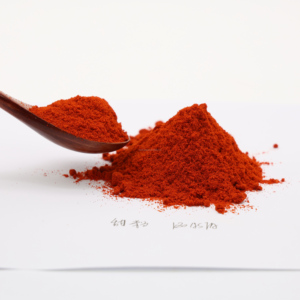
Pure Natural Taste Whole Dry Chili Chinese Dried Chili Seasoning Single Spices Herbs
Inquire Now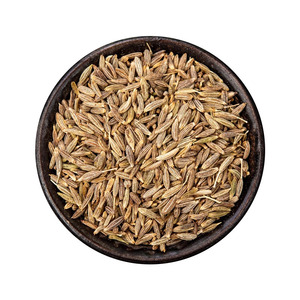
Wholesale Bulk High Quality Dried Single Spices and Herbs Whole Cumin Seeds Spices Cummin
Inquire Now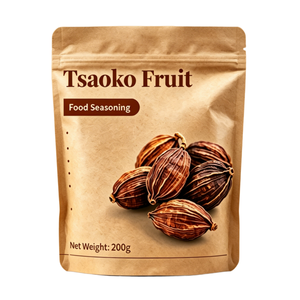
Wholesale Natural Pure Whole Tsaoko Fruit Spice for Culinary Use Ideal for Flavoring Dishes Preparations Aromatic Food Seasoning
Inquire NowIndustrial OEM/ODM Capabilities & Factory Advantages
As a tier-one contract manufacturer and bulk food ingredient supplier, we provide end-to-end operational infrastructure—spanning direct agronomic sourcing, automated cryogenic milling, steam sterilization, and private-label retail packaging.
End-to-End Contract Manufacturing (OEM/ODM)
We offer full-spectrum custom ingredient development tailored to industrial food production, commercial matrix formulation, and retail spice brand scaling.
- Custom Particle Sizing: Whole, cracked, coarse ground, or micro-pulverized fine powders (20 mesh to 120 mesh).
- Sensory & Pungency Tailoring: Custom Scoville Heat Unit (SHU) profiling for dry chili, ASTA color value adjustment, and volatile oil standardization via GC-MS testing.
- Bespoke Formulation Blending: Proprietary multi-spice brining mixes, braising blends, and marinades packed in modified atmosphere packaging (MAP).
Rigorous Food Safety & Compliance Standards
Our state-of-the-art facilities eliminate physical, chemical, and microbiological hazards to ensure total compliance with global import safety mandates (FDA, EFSA, CFIA).
- Non-Thermal & Steam Sterilization: Continuous High-Temperature Short-Time (HTST) steam sterilization to reduce TPC without degrading delicate essential oils.
- Zero-Sulfur Bleaching Guarantee: 100% natural air-drying and shade-curing processes for star anise, tsaoko, and cloves, preventing SO2 chemical residue contamination.
- Comprehensive Testing Protocols: On-site LC-MS/MS testing for pesticide residue clearance, heavy metals (Pb, Cd, As, Hg), mycotoxins (Aflatoxin B1/B2/G1/G2 and Ochratoxin A).
Global Cold-Chain & Bulk Logistics Capability
Operating integrated cold-storage units and humidity-controlled warehousing to safeguard botanical active compounds from harvest to final discharge.
- BQF Cryogenic Freezing: Block Quick Frozen (-35°C deep freezing) capability for delicate soft-texture fruits like black mulberries, preventing cellular collapse.
- Industrial Packaging Formats: Multi-ply kraft paper sacks, aluminum vacuum foil bags, 15kg/25kg fiber drums, and small retail pouches (50g to 1kg).
- Optimized Supply Chain Execution: Streamlined FOB, CIF, DDP international freight capabilities with expedited customs clearance handling.
Ingredient Standardization & Analytical Parameters
Our raw food ingredients undergo systematic physical-chemical benchmark analysis to ensure seamless batch-to-batch reproducibility for industrial food manufacturing lines.
| Ingredient Name | Processing Method | Moisture Content | Volatile Oil / Active Marker | Quality Certifications | Primary Industrial Applications |
|---|---|---|---|---|---|
| BQF Frozen Black Mulberry | Dry Brine / Cryogenic IQF & BQF (-35°C) | ≤ 82% (Natural Juice Retention) | Anthocyanin Content ≥ 2.5% | HACCP, FSSC 22000, Halal | Beverages, Dairy Fillings, Bakery, Nutraceutical Extracts |
| Whole White Pepper | Fermented Soak, Sun Dried, De-hulled | ≤ 12.0% | Piperine Content ≥ 4.0% | BRCGS, ISO 22000, Kosher | Sauce Manufacturing, Meat Curing, Snack Seasonings |
| Dried Star Anise (Sulfur-Free) | Natural Shade Cured, Hot Air Dried | ≤ 13.5% | Anethole ≥ 8.5% v/w | FDA Registered, Organic, Halal | Braising Liquids, Spice Extracts, Beverage Blends, Retort Soups |
| Whole Dried Cloves | Hand-Picked Flower Buds, Sun Dried | ≤ 11.0% | Eugenol Oil ≥ 15.0% v/w | BRCGS, ISO 9001, Kosher | Confectionery, Oleoresin Distillation, Meat Products |
| Dried Red Chili (Whole) | Dehydrated Hot Air / Sun Dried | ≤ 11.0% | Capsaicin (10,000 - 90,000 SHU) | HACCP, FSSC 22000 | Hot Pot Bases, Instant Noodle Packets, Chili Oils, Marinades |
| Whole Cumin Seeds | Machine Cleaned & Color Sorted (99.5%) | ≤ 9.5% | Cuminaldehyde ≥ 2.5% v/w | ISO 22000, Halal, Kosher | Curry Powder Formulation, Bakery Toppings, Savory Snacks |
2025–2030 Global Food Ingredient Procurement Trends
Strategic market insights for corporate procurement managers, raw material buyers, and product developers navigating supply chain shifts in botanical and agricultural commodities.
1. The Shift to Chemical-Free & Clean-Label Processing
Global food regulatory bodies (such as the European Food Safety Authority and the US FDA) have introduced stricter limits on maximum residue levels (MRLs) for chemical preservatives, sulfur dioxide (SO2), and synthetic ethylene oxide (ETO) treatments. Sulfur-free drying techniques for star anise, tsaoko fruit, and dehydrated botanicals are rapidly shifting from optional premium features to mandatory import baselines.
Commercial food brands are increasingly sourcing ingredients processed via continuous superheated steam sterilization and precision closed-loop heat pump drying to retain natural terpenes, aroma retention, and vivid visual coloration without synthetic intervention.
2. Cryogenic Preservation & Functional Fruit Matrices
Consumer demand for clean-label, functional fruit ingredients in dairy, bakery, and RTD beverage formulations has accelerated the adoption of BQF (Block Quick Frozen) and IQF (Individually Quick Frozen) dark berries, such as black mulberries. Cryogenic quick-freezing at ultra-low temperatures prevents ice crystal growth from rupturing cell structures, thereby preserving essential bio-actives like anthocyanins and natural vitamin C.
B2B procurement is moving toward pre-brined or dry-brine marinated BQF fruit blocks designed specifically for industrial pumping and automated ingredient dosing units.
3. Standardized Bio-Active & Essential Oil Specifications
Modern food processing operations require absolute consistency in taste profiles to prevent flavor drift in mass-produced packaged goods. Procurement teams are moving away from buying raw agricultural commodities purely based on visual appearance, demanding quantifiable chemical marker certificates.
High-tier food factories now mandate gas chromatography-mass spectrometry (GC-MS) verification for parameters such as Eugenol percentage in cloves, Anethole concentration in star anise, and Piperine potency in whole white pepper.
4. Supply Chain Traceability & ESG Procurement Audits
Institutional procurement strategies are prioritize suppliers with verifiable agronomic origin tracking and audited ESG (Environmental, Social, and Governance) frameworks. Direct factory-to-farm partnerships ensure fair agricultural compensation, low carbon footprint processing, and batch-level farm traceability.
Implementing strict barcode tracking from original harvesting cooperatives through cleaning, sorting, steam sterilization, and export loading provides enterprise buyers with total risk mitigation against supply chain disruptions and food fraud.
Frequently Asked Procurement & Technical Questions
Answers to common operational, regulatory, and logistics queries for B2B buyers evaluating OEM/ODM spice and ingredient suppliers.
Partner with a Leading Food Ingredients Factory
Whether you require bulk high-purity single spices, customized cryogenic frozen fruit blocks, or complete private-label seasoning lines, our engineering and procurement team is ready to support your supply chain requirements.