Featured Industrial Agricultural & OEM Ingredients
Direct-from-factory processing, rigorous grading standards, and customized packaging solutions for international importers, roasters, and food manufacturing plants.
Custom OEM Raw Peanut Kernels (Bold & Java)
Precision graded raw peanut kernels (38/42, 40/50, 50/60). Low moisture, zero aflatoxin guaranteed for industrial roasters.
Industrial Blanched Peanut Kernels (Whole & Split)
100% skinless, dry-blanched peanut kernels. Perfect for peanut butter production, confectionery, and snack manufacturing.
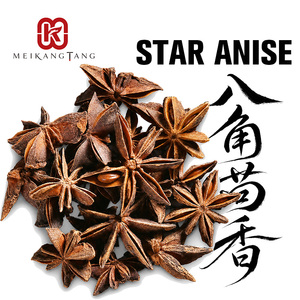
Premium Selected Sulfur-Free Dried Star Anise
Whole star anise pods processed without sulfur treatment. High essential oil concentration for beverage and seasoning formulations.
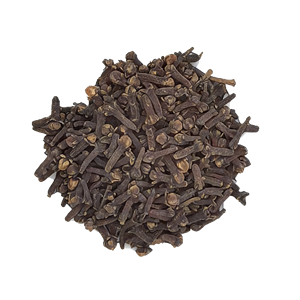
Premium Whole Cloves Natural Intense Aromatic Spice
Hand-picked dried flower buds rich in eugenol oil. Ideal for bakery blends, oleoresin extraction, and commercial marinades.
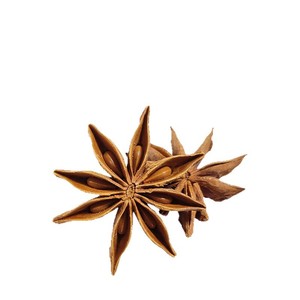
Commercial Spring-Flower Dried Star Anise Bulk Packaging
Catering and food-service grade star anise. Steam cleaned and color sorted for large-scale braised food production lines.
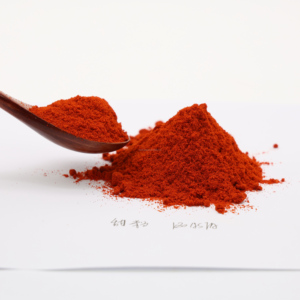
Pure Natural Sun-Dried Whole Chili Seasoning
High-capsaicin dried red chili pods. Strict moisture control (≤ 11%), stemless or with stem, optimized for industrial grinding.
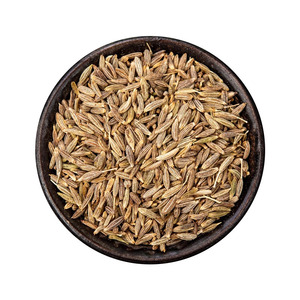
Wholesale High-Purity Whole Cumin Seeds Spices
Machine cleaned 99.5% purity cumin seeds. Uniform seed size, robust aroma, low volatile oil loss during processing.
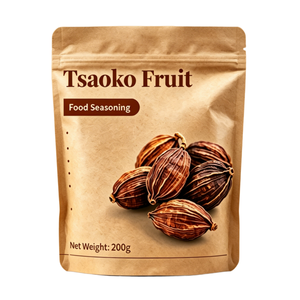
Natural Whole Tsaoko Fruit Culinary Spice
Sun-dried Tsaoko (Chinese Black Cardamom) fruit. Whole intact shells, deeply aromatic for meat processing and extract manufacturing.
Executive Whitepaper: Industrial OEM Peanut Kernel Manufacturing Matrix
An in-depth operational blueprint for enterprise procurement directors, contract packagers, and food processing engineers navigating global supply chains.
The global demand for custom OEM peanut kernels has evolved dramatically from traditional raw commodity trading into a highly specialized, specification-driven manufacturing sector. Modern food processors—spanning industrial peanut butter manufacturers, confectioners, snack food brands, and oil pressers—require raw materials engineered to precise chemical, physical, and microbiological benchmarks. Procurement decisions are no longer governed solely by metric-ton pricing; they depend on strict compliance with international phytosanitary standards, automated color sorting efficiency, mold-toxin suppression, and customizable post-harvest processing.
Agronomic Sourcing Precision
Contractual procurement directly from certified farming belts ensures varietal purity, controlled soil chemistry, and minimal seed hybridization across Bold, Runner, and Java peanut crops.
Automated Sortex Processing
Multi-spectral optical sorters (UV & Infrared) remove discolored kernels, foreign matter, and micro-cracked nuts at production speeds up to 15 tons per hour.
Aflatoxin Defensiveness
Rigorous pre-harvest moisture monitoring combined with post-harvest mechanical drying keeps Aflatoxin B1/B2/G1/G2 under strict European Union limits (< 4 ppb total).
Industrial Peanut Kernel Grading & Chemical Specification Architecture
To maintain consistent line speeds on automated roasting and grinding machinery, OEM buyers require strict compliance across physical and chemical parameters. The matrix below details factory standard benchmarks for commercial raw and blanched peanut kernel exports:
| Quality Parameter | Bold Type Kernels | Java / Runner Type | Blanched Kernels | Testing Standard / Protocol |
|---|---|---|---|---|
| Primary Size Counts (oz) | 38/42, 40/50, 50/60, 60/70 | 40/50, 50/60, 60/70, 80/90 | 38/42, 40/50, 50/60 (Split/Whole) | Count per 28.35 grams (ISO 6478) |
| Moisture Content | Max 7.0% | Max 7.0% | Max 5.0% | Air-Oven Method (ISO 665) |
| Admixture / Foreign Matter | Max 0.5% | Max 0.5% | Max 0.05% (Virtually Free) | Gravimetric Separation (ISO 658) |
| Imperfect / Damaged Kernels | Max 1.0% | Max 1.0% | Max 0.5% | Visual & Optical Sorting Audit |
| Aflatoxin (B1+B2+G1+G2) | < 4 ppb (EU) / < 15 ppb (US) | < 4 ppb (EU) / < 15 ppb (US) | < 2 ppb (EU Special Confectionery) | HPLC / Immunoaffinity Column |
| Free Fatty Acids (FFA) | Max 1.0% | Max 0.8% | Max 0.5% | Titrametric Analysis (ISO 660) |
| Oil Content (Dry Basis) | 48.0% - 50.0% | 49.0% - 52.0% | 48.0% - 51.0% | Soxhlet Extraction (ISO 659) |
Advanced OEM Processing Technologies & Custom Options
Transforming raw agricultural inputs into standardized, shelf-ready ingredients through state-of-the-art thermal, mechanical, and pneumatic infrastructure.
Pneumatic Dry Blanching & Splitting
Raw red-skin peanuts undergo low-temperature conditioning at 80°C–85°C to loosen the outer pericarp without scorching the kernel's natural oils. Rubber roller blanchers remove skins with zero chemical additives. Color sorters then isolate 100% pure white whole kernels or splits, eliminating defective nuts, unblanched seeds, and heart sprouts based on strict buyer recipes.
Custom Roasting & Particle Granulation
Continuous multi-zone belt roasters allow precise manipulation of thermal profiles—light roast for subtle confectionery applications, medium roast for standard snack lines, or dark roast for intense peanut butter aromas. Integrated roller mills produce customized peanut grits and meal (particle sizes from 1.0mm to 4.5mm) with dust-reduction sifting systems.
Global Sourcing & Procurement Trends (2025–2030 Horizon)
As environmental variability impacts major peanut-growing origins (such as India, China, Argentina, and the United States), strategic B2B sourcing is undergoing structural shifts. Procurement managers must position their supply chains to capitalize on four major macro-trends defining the next half-decade:
1. Rise of High-Oleic Cultivars
High-Oleic peanut varieties (containing oleic acid levels above 75–80% compared to standard 45–50%) offer up to 300% longer oxidative shelf life. Industrial buyers are shifting contract volumes to High-Oleic OEM suppliers to eliminate synthetic antioxidants (BHA/BHT) from clean-label snack and butter formulas.
2. IoT-Monitored Cold-Chain Ocean Shipping
Transit mold formation (Aspergillus flavus) during multi-week ocean transport is being neutralized through smart containerization. Leading suppliers deploy real-time relative humidity (RH) telemetry, desiccants, and vacuum-sealed liner bags (25kg & 1000kg Big Bags) to maintain moisture stability below 6.5%.
3. Hyper-Stringent Heavy Metal & Chemical Residue MRLs
Regulatory authorities in the EU, Japan, and North America have reduced Maximum Residue Limits (MRLs) for pesticides like Chlorpyrifos and heavy metals like Cadmium. Modern OEM factories must provide batch-level LC-MS/MS laboratory certificates prior to port departure.
4. Blockchain Traceability from Field to Factory Gate
Enterprise buyers are prioritizing transparent supply chains. Digital batch tracking links finished pallet QR codes directly to farm-level harvesting data, pesticide application logs, and sheller lot numbers, providing full ESG accountability.
Manufacturing Infrastructure & Factory Capabilities
Combining decades of agricultural processing heritage with modern food safety management systems to serve contract buyers worldwide.
Our manufacturing ecosystem operates on an integrated processing model. By controlling every stage—from direct farm contract procurement and sheller screening to double optical color sorting, mechanical blanching, and vacuum packaging—we eliminate middleman markups while ensuring zero-defect quality control.
Fully Certified Facilities
Operating under ISO 22000, HACCP, BRCGS, Halal, and Kosher certifications. Regular third-party factory audits by SGS, Intertek, and Cotecna guarantee global compliance.
Scalable Supply Capacity
Processing over 550,000 metric tons of agricultural raw materials annually, supported by 10,000 MT climate-controlled warehouse storage to prevent seasonal price spikes.
Custom Packaging Flexibility
Offering 25kg vacuum-sealed poly-lined bags, 50kg jute bags with inner PE liners, 1000kg FIBC Big Bags with nitrogen flushing, and custom private-label retail pouches.
Frequently Asked B2B Procurement Questions (FAQ)
Direct technical answers to common questions asked by international commodity buyers, quality managers, and supply chain executives.
What is the minimum order quantity (MOQ) and standard lead time for OEM orders?
Our standard minimum order quantity (MOQ) for custom OEM raw or blanched peanut kernels is 1 FCL (Full Container Load - approx. 19 to 25 Metric Tons depending on packaging type). Lead time for processing, optical sorting, laboratory sampling, and container stuffing is typically 10 to 15 business days following LC opening or deposit receipt.
How does your factory ensure compliance with strict European Union Aflatoxin regulations?
We implement a multi-barrier defense strategy: (1) Farm-level pre-harvest soil treatments and timely drying; (2) Mechanical pneumatic cleaning and UV optical sorting to eliminate moldy kernels; (3) In-house HPLC laboratory batch analysis; and (4) Mandatory pre-shipment inspection and certification by accredited third-party laboratories (SGS / Bureau Veritas) confirming total Aflatoxin < 4 ppb and Aflatoxin B1 < 2 ppb.
What is the structural difference between Bold and Java kernels for peanut butter production?
Bold type kernels are elongated with a darker reddish skin and higher oil concentration (~50%), providing a robust, roasted flavor ideal for crunchy spreads and snack packs. Java (Runner) kernels are spherical with a pink skin and uniform shape, making them ideal for high-speed automated grinding machines to achieve ultra-smooth peanut butter texture with minimal oil separation.
Can you provide custom roasting profiles and custom cut sizing (grits)?
Yes. Our thermal processing lines feature continuous multi-stage roasters capable of matching Agtron color scale parameters specified by the client. Our industrial milling equipment produces custom-sized peanut granules (ranging from 1.0mm to 4.5mm) with zero-dust air-sifting for bakery, ice cream topping, and confectionery integration.
What ocean packaging options exist to prevent oxidation and moisture damage during sea freight?
We recommend 25kg multi-layer vacuum bags with EVOH oxygen barrier film, packed inside cardboard outer cartons or master bags. For bulk industrial use, we offer 1000kg FIBC Big Bags equipped with inner aluminum foil liners and nitrogen gas flushing, effectively maintaining oxygen levels below 0.5% and preserving freshness for up to 24 months.
What commercial trade terms (Incoterms) and payment methods do you support?
We operate across major Incoterms 2020 including FOB (Free on Board), CFR (Cost and Freight), and CIF (Cost, Insurance, Freight) to any major global port. Standard payment terms include Irrevocable Letter of Credit (L/C at sight) issued by a top-tier international bank, or Telegraphic Transfer (T/T) with a 30% advance deposit and balance payable against presentation of shipping documents.
Partner with a Trusted OEM Peanut Kernel Manufacturer
Streamline your industrial supply chain with factory-direct pricing, custom grading specifications, and guaranteed international phytosanitary compliance. Contact our B2B export engineering team today for instant technical consultations, batch samples, and competitive FOB/CIF quotations.