Strategic B2B Buyer’s Guide: China Wholesale Rice Manufacturing & Global Export Landscape
As global agri-food supply chains undergo structural shifts driven by geopolitical recalibrations, freight rate volatility, and evolving dietary preferences, institutional purchasers require unprecedented clarity when sourcing from a China Wholesale Rice Factory. Sourcing commercial rice at bulk enterprise scale involves navigating complex variables—including grain geometry, amylose content, gelatinization temperature profile, milling yield ratios, and strict phytosanitary compliance standards. China stands as one of the world's most technologically advanced processing hubs for processed, value-added, and staple grain exports, blending high-yielding agricultural production with state-of-the-art European milling machinery.
Whether you are procuring long-grain fragrant Jasmine rice for commercial retail distribution, specialized Calrose medium grain for food-service sushi production, high-anthocyanin Black Pearl specialty rice, or precooked instant bases for self-heating MRE meal manufacturers, understanding factory specs is paramount to protecting margin and brand reputation.
Key Technical Parameters in Commercial Rice Specification & Grading
Professional grain buyers must evaluate wholesale supplies against established international metric standards to prevent quality degradation during transcontinental shipment. The primary technical metrics engineered within our manufacturing plants include:
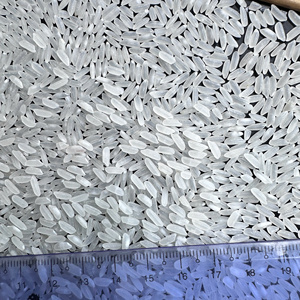
- Broken Kernel Thresholds (1% to 25%): Standardized using rotary mechanical sieves and optical thickness graders. For premium culinary applications (such as Grade-1 Jasmine or Premium Sushi Rice), broken ratios are strictly maintained under 5%, preserving grain structural integrity during cooking.
- Milling Degree & Whiteness Index: Measured via Kett whiteness meters. High-milled white rice undergoes multi-stage abrasive polishers and water polishers to achieve high-luster kernel surface aesthetics while retaining structural endosperm toughness.
- Amylose Percentage & Cooking Texture: Amylose content directly dictates sticky versus fluffy properties. Low amylose grains (1%-2% in Glutinous rice) produce characteristic sticky elasticity; medium amylose (15%-20% in Calrose/Jasmine) offers soft moist cohesion; high amylose (>23%) yields dry, separate grains optimal for industrial canning and fried rice preparations.
- Fumigation and Moisture Thresholds: Moisture levels are calibrated to climate destination requirements. Trans-equatorial freight demands moisture control under 13.5% alongside aluminum phosphide fumigation treatment compliant with USDA and EU EFSA regulations.
Comparative Technical Specifications Matrix Across Product Categories
| Grain Category | Typical Moisture | Broken Ratio Options | Amylose Content | Primary Industrial / Retail Application |
|---|---|---|---|---|
| Jasmine Fragrant Rice | 12.5% - 13.5% | 1%, 5% max | 14% - 17% | Premium Retail Brands, Ethnic Food Import, Catering |
| Calrose Medium Grain | 13.0% - 14.0% | 3%, 5% max | 18% - 21% | Japanese / Korean Foodservice, Sushi Manufacturing |
| Black Pearl Rice | 12.0% - 13.0% | 2%, 5% max | 16% - 19% | Nutraceuticals, Premium Specialty Retail, Health Foods |
| AHAX Precooked Rice | 6.0% - 8.0% | N/A (Processed) | Modified (Gelatinized) | Self-Heating Meal Kits, Emergency Rations, Instant Foods |
| Glutinous Sticky Rice | 13.0% - 14.0% | 5%, 10% max | 1% - 2% | Asian Snack Manufacturing, Desserts, Processed Foods |
Future Market Trends & Procurement Outlook (2025–2030)
The global rice export trade is experiencing rapid modernization. Enterprise procurement leads and procurement directors must align their multi-year strategies with four emerging megatrends shaping factory operations across Asia:
1. Exponential Growth in Precooked & Convenience Formats
The rapid rise of instant self-heating hot pots, fast-casual food systems, and military-grade MRE meal kits has accelerated international demand for pre-gelatinized, high-speed rehydration rice. Advanced processing facilities now utilize fluidized-bed drying and steam cooking technologies to manufacture shelf-stable precooked rice bases (such as AHAX Precooked 10kg bulk bags) that fully rehydrate in under 8 minutes with boiling water or self-heating reaction bags. Institutional buyers are shifting away from raw grain processing toward pre-treated grains to minimize local culinary prep labor and energy expenditures.
2. Expansion of Functional & High-Nutrient Grains
Consumer demand for natural health products has pushed specialty varieties like Black Pearl Rice into mainstream global supermarket chains. Rich in natural anthocyanins, antioxidants, dietary fiber, and essential minerals, black rice commands higher profit margins per metric ton compared to standard white long grain. Forward-thinking wholesale distributors are increasingly securing exclusive OEM contracts for private-label pigmented rice varieties directly from certified origin factories.
3. Digital Traceability & Sustainable Farm-to-Port Operations
International environmental regulations (including EU deforestation and carbon footprint disclosures) are driving rice milling facilities to implement blockchain-enabled batch tracking. Modern suppliers provide end-to-end transparency—linking specific grain shipments back to precise agricultural cooperatives, tracking fertilizer input metrics, water usage efficiency during cultivation, and solar power consumption ratios within the milling facility.
4. Automated Packaging Automation & Vacuum Shelf Preservation
To mitigate infestation risk and preserve delicate volatile aromatic compounds (such as 2-acetyl-1-pyrroline in Jasmine varieties), wholesale packaging is shifting from traditional burlap or simple single-layer woven bags to high-barrier vacuum nitrogen-flushed packaging. Factory-installed automated packing lines can now produce hermetically sealed bricks from 1kg to 10kg at speed, ensuring 24-month shelf life without chemical preservatives.