Featured Export Products & Botanical Ingredients
Explore our factory-direct bulk portfolio engineered for international food manufacturers, spice importers, and botanical extractors requiring strict European CE compliance and phytosanitary purity.
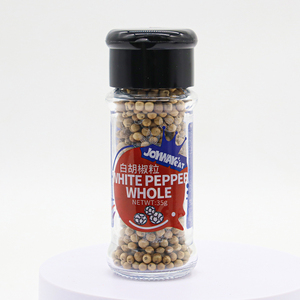
Small Packaged White Pepper Whole Spices 50g Dried Spicy Food Seasoning for Cooking
Contact Us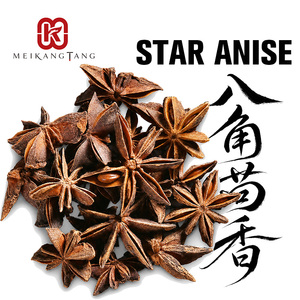
Premium Selected Sulfur Free Dried Star Anise For Cooking Seasoning,Marinating Ingredients And Spices Herbs Products
Contact Us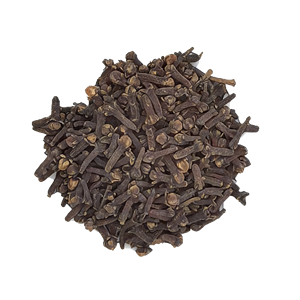
Premium Whole Cloves Natural Intense Aromatic Spice Dried Flower Buds for Cooking Baking Marinating Beverage Blends
Contact Us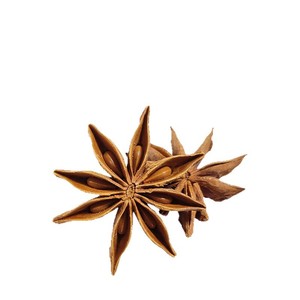
Spring-flower Star-anise Sulfur-free Whole Dried Spices Wholesale Braised-food Seasoning Catering Commercial Use Packaged Food
Contact Us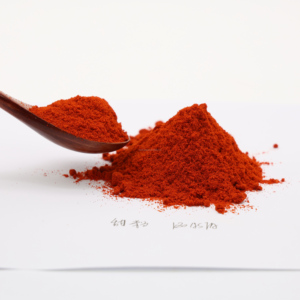
Pure Natural Taste Whole Dry Chili Chinese Dried Chili Seasoning Single Spices Herbs
Contact Us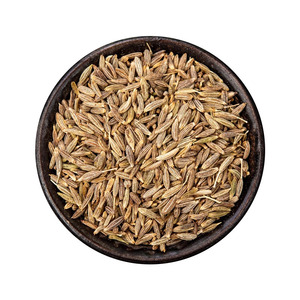
Wholesale Bulk High Quality Dried Single Spices and Herbs Whole Cumin Seeds Spices Cummin
Contact Us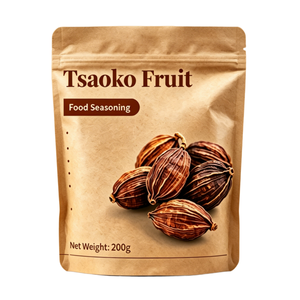
Wholesale Natural Pure Whole Tsaoko Fruit Spice for Culinary Use Ideal for Flavoring Dishes Preparations Aromatic Food Seasoning
Contact UsIndustrial Scale & Quality Verification Framework
Operating as a primary manufacturer of CE certified black sesame seeds and agricultural food ingredients, our processing infrastructure integrates state-of-the-art optical cleaning, cold-chain preservation, and micro-contaminant screening.
550,000+
Meters/KG Annual Capacity
4,500+
Lab Batches Verified Yearly
99.9%
Optical Purity Standard
20+
Export Destined Nations
Engineering Excellence in Black Sesame Manufacturing
In global agro-commodity processing, the designation of a CE Certified Black Sesame Manufacturer & Factory extends beyond standard agricultural aggregation. It signifies an end-to-end, industrial-grade processing ecosystem certified under European conformity guidelines for food contact machinery, safety systems, and strict hazard prevention protocols. Black sesame seeds (Sesamum indicum) represent one of the most chemically dense oilseeds utilized across global culinary, pharmaceutical, and cosmetic supply chains. However, raw harvest sesame contains variable levels of organic debris, dust, heavy metals, micro-biological pathogens, and residual moisture that threaten product stability and end-user compliance.
Our manufacturing facility resolves these supply chain vulnerabilities through an automated, five-stage purification architecture engineered specifically for premium black sesame seeds. By deploying specialized multi-channel CCD color sorting technology, infrared density separation, high-frequency sieve grading, and continuous dry-steaming micro-sterilization, we deliver black sesame seeds characterized by uniform charcoal pigmentation, high sesamin concentration, and absolute chemical compliance with international food regulations.
Information Gain Insight: Standard commodity black sesame often suffers from color contamination (admixture of white or immature reddish seeds) and micro-toxin retention. Our factory employs double-pass chromatic sorters capable of detecting color variance within a 0.02mm resolution, achieving an industry-leading 99.9% color purity score essential for high-end confectionery, baking, and pharmaceutical lipid extraction.
Comprehensive Quality Assurance & Chemical Specification Matrix
To provide corporate procurement managers with absolute technical clarity, the following table delineates our standard benchmark parameters for high-purity black sesame seeds processed in our CE-compliant factory:
| Quality Parameter | Standard Commercial Grade | Our CE Factory Benchmark | Testing & Verification Protocol |
|---|---|---|---|
| Purity / Cleanness | 98.5% - 99.0% | ≥ 99.90% (Sortex Cleaned) | ISO 658 / Visual Optical Scan |
| Moisture Content | 6.5% - 8.0% | ≤ 5.0% (Moisture Stabilized) | ISO 665 Vacuum Oven Drying |
| Oil Content (Dry Basis) | 42% - 46% | ≥ 48% - 52% | Soxhlet Extraction Method |
| Free Fatty Acids (FFA) | < 2.0% | ≤ 1.0% | ISO 660 Titration Method |
| Sesamin Concentration | 0.30% - 0.40% | ≥ 0.55% - 0.65% | HPLC Assay Chromatography |
| Ethylene Oxide (ETO) | Variable / Uncontrolled | Non-Detected (< 0.01 mg/kg) | GC-MS Screening (EU Compliant) |
| Heavy Metals (Pb, Cd) | Within Regional Limits | Lead <0.1mg/kg, Cadmium <0.05mg/kg | ICP-MS Spectrometry |
| Microbiological Load | Standard Colony Counts | Salmonella: Absent / 25g, TPC < 10,000 CFU/g | Dry Steam Pasteurization Protocol |
Five-Stage Industrial Processing Architecture
Achieving consistent technical specifications requires an uncompromising mechanical workflow. Our factory operates under strict HACCP and ISO 22000 manufacturing guidelines, utilizing equipment designed to meet CE safety and sanitary standards:
1. Pre-Cleaning & De-Stoning
Multi-layer vibrating screen sieves remove macro-impurities (twigs, leaves, pods), followed by high-density gravity de-stoners that eliminate micro-stones and mineral particles identical in size to sesame seeds.
2. Optical Chromatic Sorting
Dual-camera monochrome and full-color Sortex systems analyze every individual seed in real-time, ejecting off-color white, yellow, or damaged seeds to guarantee uniform deep black visual aesthetics.
3. Thermal Moisture Stabilization
Controlled low-temperature indirect air drying reduces free seed moisture below 5.0%. This prevents enzymatic lipid hydrolysis, inhibiting Free Fatty Acid (FFA) elevation during transatlantic ocean freight.
Future Sourcing & Global Procurement Trends (2025–2030)
Strategic procurement directors in food production, retail packaging, and nutraceutical industries face evolving market forces. As regulatory bodies enforce stricter chemical oversight and consumers demand transparent supply chains, black sesame procurement is shifting rapidly from spot-market commodity buying to integrated contract manufacturing. Key global trends shaping the next decade include:
1. Rigorous Ethylene Oxide (ETO) & Pesticide Controls
European and North American border authorities have intensified customs sampling for ETO sterilization residues and neonicotinoid pesticides. Importers are abandoning unverified traders in favor of CE certified manufacturers offering full gas chromatography-mass spectrometry (GC-MS) batch validation prior to port shipment.
2. Rise of Functional Food & Nutraceutical Extraction
Black sesame is increasingly valued for its high concentrations of lignans—specifically sesamin and sesamolin—which exhibit potent anti-oxidative and liver-protective properties. Demand for high-oil, high-lignan black sesame strains suitable for supercritical CO2 extraction is projected to grow at a CAGR of 7.4% through 2030.
3. Sustainability & Full Traceability Commitments
ESG compliance now dictates raw material sourcing. Global food brands require farm-to-factory traceability, verified non-GMO cultivar integrity, and eco-friendly vacuum-sealed barrier packaging that reduces plastic waste while extending shelf life up to 24 months without chemical preservatives.
Technological Innovations in Black Sesame Processing
The evolution of industrial seed processing technology is creating significant competitive advantages for forward-thinking food brands. As a direct manufacturer, our facility actively integrates next-generation processing engineering to maximize yield, preserve natural aromas, and guarantee biosecurity.
AI-Enhanced Optical Sorting
Traditional mechanical sieves fail to detect subtle seed defects. Deep-learning visual inspection algorithms analyze grain shape, luster, and color spectrum at ultra-high speeds, separating premium food-grade black sesame from inferior sub-grades with 99.9% accuracy.
Cold Continuous Steam Sterilization
Replacing chemical fumigants, continuous dry-steam pasteurization eliminates human pathogens (E. coli, Salmonella) within seconds without raising core oil temperatures. This preserves heat-sensitive sesamin compounds and maintains raw natural organoleptic profiles.
Controlled Atmosphere Packaging (CAP)
To eliminate oxidation during long-distance maritime transport, bulk products are flushed with food-grade nitrogen gas in heavy-duty aluminum-laminated bags, preserving crisp texture, aromatic oils, and zero rancidity upon container unloading.
Frequently Asked Questions for B2B Buyers
Direct answers to essential technical, logistical, and compliance questions asked by corporate procurement managers and quality assurance teams:
Q1: What specific certifications does your factory hold for European & North American imports?
Our manufacturing facilities operate under certified ISO 22000:2018 food safety management systems, HACCP verification, and FDA registration. Our processing line compliance holds valid CE documentation for industrial machinery and hygienic production standards, ensuring our black sesame products fully conform to EU Regulation (EU) 2023/915 regarding maximum levels for contaminants.
Q2: How do you guarantee zero Ethylene Oxide (ETO) contamination in bulk sesame shipments?
We do not utilize chemical gas fumigation or ETO treatments at any stage of our storage or processing. Microbial decontamination is conducted strictly through thermal steam pasteurization or certified irradiation upon client request. Every export batch undergoes independent GC-MS analysis at accredited 3rd-party laboratories (e.g., SGS, Eurofins) to confirm non-detectable ETO levels (<0.01 mg/kg) prior to customs declaration.
Q3: What is the difference between natural black sesame and hulled black sesame?
Natural black sesame retains its dark, mineral-rich outer seed coat (hull), which contains high fiber, calcium, and distinct aromatic bitterness favored in baking, paste grinding, and traditional food preparations. Hulled black sesame has the outer hull mechanically removed, yielding a softer seed suitable for specialty oil extraction and refined culinary applications. We supply both specifications in bulk volumes.
Q4: What are your standard bulk packaging options for global ocean freight?
We offer robust B2B packaging options tailored to ocean transit conditions, including: 25kg multi-wall craft paper bags with internal PE liner, 50kg PP woven sacks, 1,000kg FIBC Jumbo Bags, and 15kg/25kg nitrogen-flushed vacuum foil packs for extended shelf-life preservation. Custom OEM branding and labeling are fully supported.
Q5: What is your Minimum Order Quantity (MOQ) and production turnaround time?
Our standard MOQ for full-container-load (FCL) shipments is 1 x 20ft container (approx. 18 to 19 metric tons depending on packaging style). For trial orders or specialized single-spice portfolio combinations, we accommodate LCL shipments starting from 3 to 5 metric tons. Factory dispatch is typically completed within 10 to 14 business days post L/C or deposit confirmation.
Q6: How is sesamin purity and oil yield verified for nutraceutical clients?
For buyers seeking high-potency extraction stock, we conduct High-Performance Liquid Chromatography (HPLC) testing on raw seed samples to quantify active lignan markers (Sesamin & Sesamolin). Batch-specific Certificate of Analysis (COA) documentation accompanies every shipment detailing moisture, oil content percentage, peroxide value, and FFA levels.
Q7: Can you supply mixed-container shipments containing other spices and herbs?
Yes. We specialize in consolidated B2B ingredient sourcing. Importers can combine CE certified black sesame seeds with other key spices from our catalog—such as Star Anise, Whole Cloves, Cumin Seeds, White Pepper, and Dried Chili—within a single container to optimize freight costs and inventory management.
Q8: What quality control steps prevent aflatoxins and mycotoxins?
Aflatoxins are controlled at the cultivation and drying origin through humidity-monitored warehousing. Upon arrival at our facility, incoming seed lots are screened via ELISA testing. Final processed seeds undergo strict moisture containment below 5.0% to prevent fungal growth during storage, ensuring Aflatoxin B1 + B2 + G1 + G2 total levels remain well under 4.0 μg/kg (EU regulation limits).
Why Direct Factory Contract Manufacturing Wins
Bypassing commodity intermediaries and securing direct supply contracts with an established factory provides global food enterprises with significant strategic advantages. Over years of dedicated export operation, our manufacturing framework has consistently delivered value through transparent pricing, customized specifications, and uncompromised quality assurance.
Rigorous Traceability & E-E-A-T Standards
Our enterprise enforces full batch traceability. Every container leaving our plant carries complete documentation tracing raw harvest origin, cleaning logs, color sorter calibration records, and third-party laboratory verification certificates.
Flexible OEM / Private Label Packaging
We provide complete private label packaging lines for commercial distributors, catering suppliers, and retail brands. From 50g small food-service packs to heavy-duty industrial vacuum bags, our packaging machinery operates under strict hygienic controls.
Direct Factory Pricing & Contract Hedging
By controlling primary processing, we offer stable multi-quarter fixed pricing contracts. This insulates our international corporate partners from speculative market spikes in agricultural commodities while maintaining guaranteed product volume access.
Request Factory-Direct Quotations & Technical Samples
Connect directly with our engineering and procurement team. We provide complimentary laboratory testing samples, customized technical spec sheets, and firm CIF/FOB pricing for your upcoming production cycles.
Contact Us